
What Is MES System?
What is MES? A manufacturing execution system (MES) is software used to manage, monitor and record production on the shop floor. It connects production orders and production schedules with information about raw materials, operations and quality, using data from machines, operators and other systems to give manufacturers real-time visibility into shop floor operations, improve efficiency and help ensure products meet quality standards.
MES systems monitor and control manufacturing operations in real time, providing real-time visibility into manufacturing operations and detailed tracking of manufacturing processes.
MES systems monitor and control manufacturing operations in real time, providing real-time visibility into manufacturing operations and detailed tracking of manufacturing processes.
MES helps teams answer practical questions: How far has an order progressed? What is delaying it? Which material lots were used? For manufacturing companies running complex shop floors, multiple plants, or a mix of legacy and modern equipment, that visibility is critical for reducing downtime, improving quality, supporting compliance and making better day-to-day production decisions.
This article explains what MES does, how it differs from ERP, OEE and SCADA, where it improves and where it falls short, what affects implementation and cost, how to compare MES software, and why it plays a central role in operational excellence and digital transformation.
MES System Overview
What does MES stand for?
MES stands for Manufacturing Execution System. The term refers to software that supports the execution and recording of manufacturing operations. You may also see the phrases MES software, MES system and manufacturing execution software used for this category.
What does a manufacturing execution system do?
Production information is often spread across paper records, spreadsheets and machine readings. MES brings those records into the context of the manufacturing process: an output count belongs to an order, a raw-material lot belongs to a batch, and a quality-control result belongs to an operation.
Supervisors use this information to follow progress. Operators access instructions and record work. Quality teams review process history when investigating a problem. When the necessary connections are available, MES can give teams near-real-time visibility into production status. It does not make incomplete or inaccurate data reliable automatically; data definitions, collection rules and ownership still matter.
How does MES work? A production order example
Consider a parts manufacturer running an order through several operations and an inspection. This simplified example shows how mes works by collecting data about production activities across the workflow, rather than a specific customer deployment.
Depending on the architecture, MES may exchange data with ERP, PLC or SCADA, quality, warehouse and other business systems. The useful question is which information must move between systems, how often it should be updated, and who owns the data when a connection is unavailable. Supervisors can follow production progress on the factory floor and use that information to make informed decisions, while connected data can also reveal machine performance and support product quality.
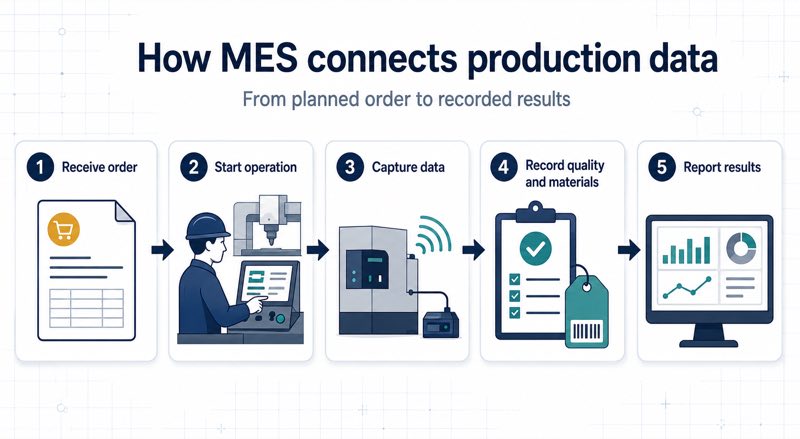
Receive the production order
The order enters MES, for example through an ERP integration. Under ISA-95, MES sits at Level 3 between enterprise systems and control systems. It includes the product, planned quantity and information needed to carry out the operations, while linking with other enterprise systems to support production planning.
Start the operation
The operator selects the task and records its start. Depending on configuration, MES provides the relevant work instructions and checks the materials assigned to the workstation, which is especially useful in regulated industries. When the order enters MES through ERP integration, it also supports production planning between enterprise systems and lower-level control systems with visibility across the entire production process.
Capture real time data and execution data
Machine readings provide operating status and output counts, which helps flag potential issues early. In regulated industries, these checks help maintain visibility across the entire production process at the workstation level. The operator adds information the machine cannot identify, such as the reason for a stoppage, supporting production efficiency.
Record quality and material history
Inspection results are linked to the relevant operation or batch, and machine readings can also highlight potential issues that affect production efficiency as part of quality management. Material records connect incoming lots to the finished product, supporting later investigation.
Complete the work and report results
The team reviews completed work. Agreed results, such as output quantities, material consumption, and inspection results as part of quality management linked to the relevant operation or batch, can return to ERP and other enterprise systems for planning and reconciliation, giving teams a comprehensive view.
What are the main MES functions, including production scheduling?
Typical MES functions include managing production operations across factory floor operations and sharing execution data upward:
- Production scheduling, order execution and work-in-progress tracking
- Production and machine data collection, including near-real-time status where connected
- Material traceability and product genealogy
- Digitale Arbeitsanweisungen, quality control and in-process records
- Downtime analysis, production performance and reporting
The exact combination varies between products and implementations. Some systems connect to maintenance, inventory or resource-management modules, while others keep those processes in separate applications. When results return to ERP, sharing that data with other enterprise systems can provide a more comprehensive view for planning and reconciliation. Compare the operational coverage, data flow and ownership of each system rather than relying on the product label alone.
MES vs ERP: what is the difference?
Enterprise resource planning (ERP) covers business processes such as purchasing, finance, inventory control, planning and human resources. MES functions support production operations and connect factory floor operations with execution records and reporting. Integration allows business plans and reporting to use actual results from the shop floor.
The boundaries can overlap. Some ERP products include extensive manufacturing capabilities. Before adding MES, identify which requirements your current system already meets and where execution data or process support is missing.
| Comparison | ERP | MES |
|---|---|---|
| Primary focus | Business resources and transactions | Shop floor execution |
| Example records | Orders, material requirements, costs | Operation status, events, batch history |
| Example use | Plan and account for an order | Record how the order was produced |
MES vs OEE: a system and a performance measure
Gesamtanlageneffizienz (OEE) is a measure based on availability, performance and quality. OEE monitoring software measures those factors and helps teams investigate losses. MES covers production execution more broadly, including functions such as order tracking and material history.
If the immediate need is to understand machine stoppages, OEE monitoring may be a useful starting point. If the need also includes linking operations to materials and quality results, assess the relevant MES capabilities.
Manufacturing operations management (MOM) describes the broader management of manufacturing operations, including production, quality, maintenance and inventory operations. MES refers to software for production execution. Vendors use these terms in different ways, so compare process coverage and capabilities rather than relying on the product label alone.
What are the benefits of MES software?
MES can make production information available sooner and reduce repeated manual entry when data is captured at the source, helping businesses improve operational efficiency. A connected material and process history helps quality teams investigate issues, while execution data allows production teams to compare plans with actual results and support operational excellence for customers.
Measure outcomes against a baseline to track productivity and increased efficiency. Useful KPIs might include reporting time, the time needed to retrieve batch history, data completeness, order completion performance, OEE, first-pass yield, and scrap rate. Account for changes in product mix, production load, and metric definitions when comparing results to increase productivity.
What are the limitations of MES?
Software does not repair equipment or correct inaccurate master data on its own. A downtime report still needs someone to investigate the cause and take action. Missing material records also limit the usefulness of product genealogy.
An implementation therefore needs clear rules for collecting data, maintaining its accuracy and responding to deviations. Define who uses each report and which decision it supports. A dashboard has limited value if no one owns the next action.
Does MES replace machine control systems?
MES usually works with the automation layer and consumes its data. It does not replace the machine control or safety functions performed by controllers and dedicated safety systems. The responsibilities of each layer should be clear in the system design.
MES vs SCADA: what is the difference?
Supervisory control and data acquisition (SCADA) systems focus on monitoring and supervisory control of equipment and processes. MES focuses on production execution: orders, operations, materials, quality records and production results. In many plants, SCADA and MES work together, with clear boundaries for control, data collection and operational decisions.
SCADA does not automatically provide the order, batch or genealogy context that an MES may manage, while MES does not replace controller or safety functions. The right architecture depends on the process, data sources and required response time.
How should a manufacturer prepare for MES?
Choose the operational problem and initial production area based on your industry requirements and define how you will measure progress.
Document normal operations and exceptions, including rework, material substitutions, and order changes, to match the scope of systemu MES to actual processes and planning needs.
Identify data sources across machines, operator interfaces, connected business systems, and SCADA so teams have a real-time view of equipment while MES tracks execution status.
Agree on IT responsibilities, user access, and how production should operate during connectivity interruptions.
Test real scenarios with operators and define acceptance criteria before go-live.
How much does MES software cost?
MES cost depends on the software scope, number of workstations or sites, integration work and equipment readiness. A budget should cover software, hardware, implementation, training and ongoing support. Compare the total cost over the same period and for the same scope.
For international deployments, confirm the quotation currency, regional service coverage and any site-specific work. A shared software platform does not mean every plant has the same process, infrastructure or deployment effort.
Wie lange dauert die MES-Einführung?
There is no single timeline that applies to every MES project. A machine-data pilot, the first production go-live and a full plant rollout are different milestones. Scope, integrations, data readiness and the time available for testing and training affect the schedule.
When evaluating a proposed timeline, ask what will be operational at the end, when the clock starts and which prerequisites the manufacturer must provide. For multiple sites, distinguish the initial deployment from later rollouts and local adaptations.
How do you compare MES solutions?
Ask suppliers to demonstrate a real production scenario, including an exception such as rework or an incorrect material. Check which capabilities are included, which require additional modules, and how integrations and ongoing changes will be supported.
Frequently asked questions about MES
Can MES work without ERP?
Yes, if the required information is available from other sources or entered into MES. ERP integration is a method of exchanging data, rather than a prerequisite for MES to function.
Does all MES data have to come directly from machines?
No. MES can combine automatic readings with operator reporting. Define which information can be captured automatically and which requires human input or confirmation.
Is MES suitable for smaller manufacturers?
Company size is only one consideration. Process complexity, traceability needs and the cost of the current way of working matter too. Match the scope to a specific operational need.
Can an ERP system include MES functions?
Some ERP platforms include manufacturing capabilities, and some organizations use connected MES functions within an ERP product. That does not make every ERP deployment equivalent to an MES. Compare whether the system supports production execution, real-time data capture, work instructions, quality records and material genealogy for your process.
Does MES guarantee an improvement in OEE?
No fixed improvement applies to every implementation. MES data can help identify losses, but results also depend on the actions taken and the production conditions.
Explore these capabilities in Accevo MES
Evaluating software for your plant? Explore Accevo MES features, ERP and machine integration, and the process for defining an implementation scope.