包装行业软件


What is software for the packaging industry?
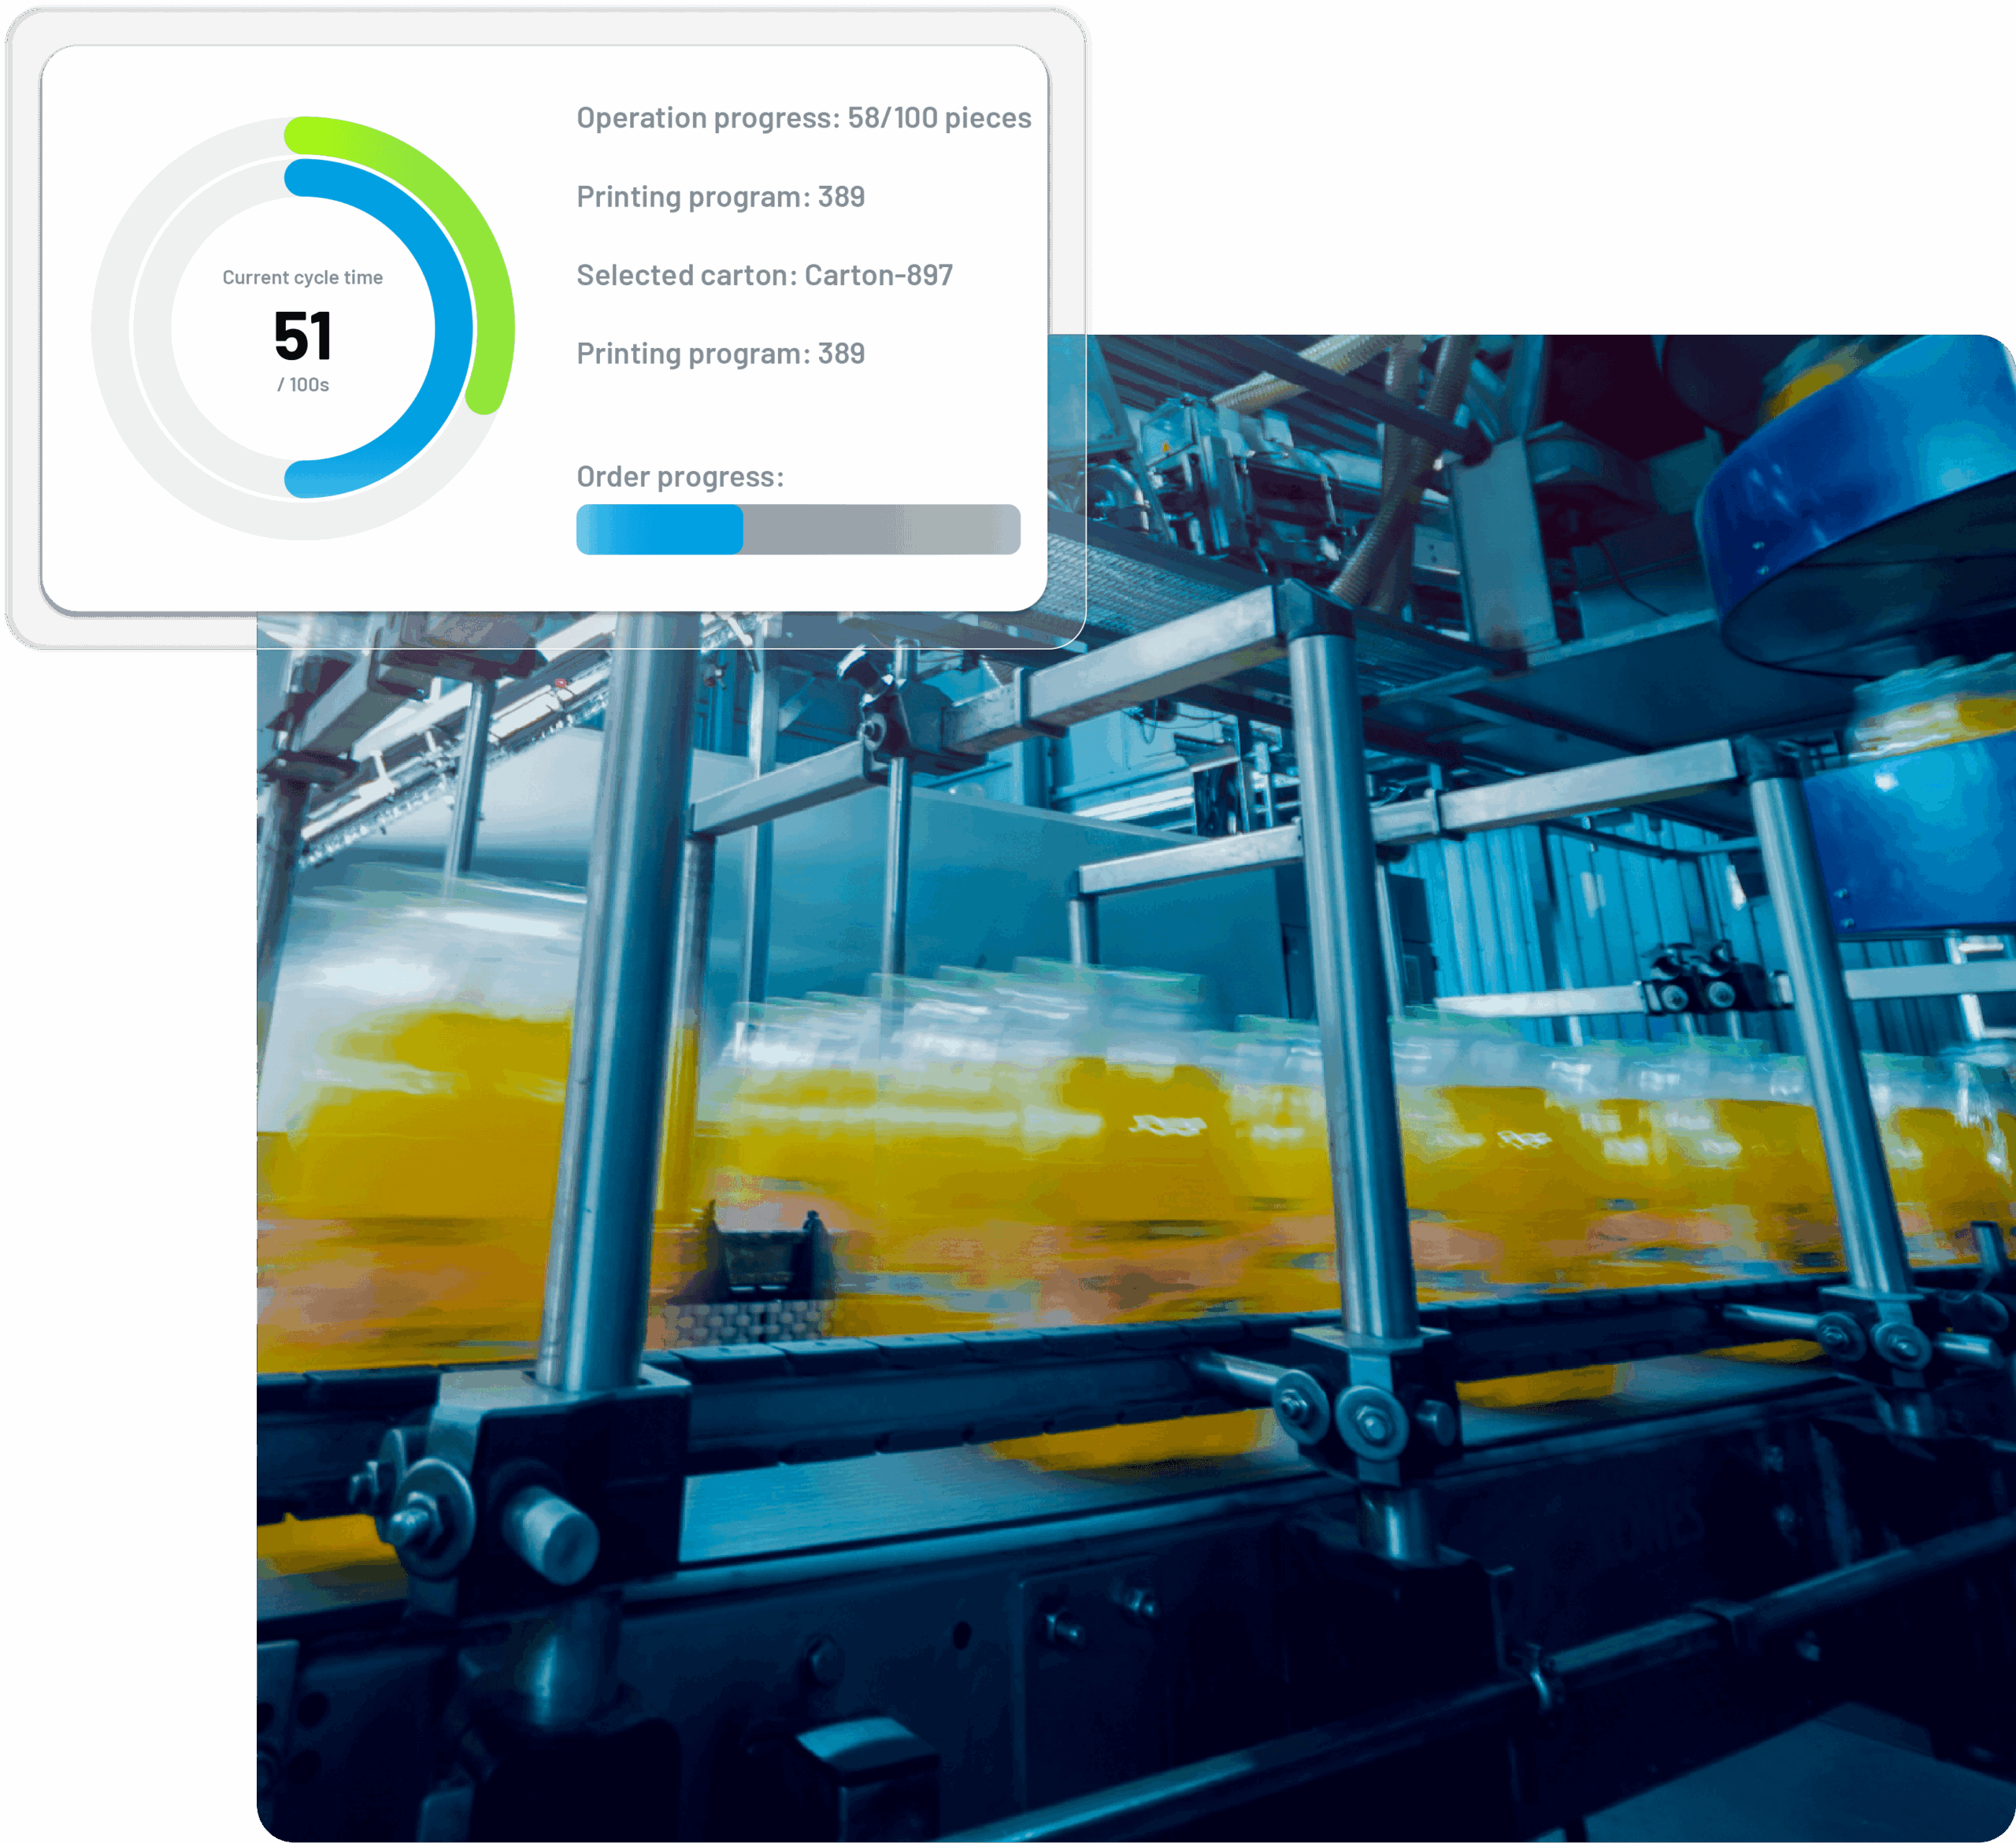
Software for the packaging industry means production monitoring and execution built around the way packaging lines actually behave: a chain of machines running at speed, where one station stopping for eight seconds starves everything downstream and nothing gets written down.
This is a different problem from packaging design software. Nothing on this page draws a carton. What it does is measure and improve the line that fills it – OEE, stop reasons, changeover duration, speed loss and reject rate – and keep a consistent view of output across shifts, lines and sites.
Packaging lines rely on a mix of automation and operator actions, so the system has to cover both: machine and line events read from the controllers, plus operator input for the reasons no PLC can supply. Performance is then tracked with real production context – which order, which SKU, which crew.

Where packaging lines actually lose output
Ask three people why a packaging line missed target and you will get three answers. The loss categories below are the ones that dominate in practice, and each of them is invisible without automatic measurement.
Stops and microstops
微停机 – jams, misfeeds and brief starvation lasting seconds. Individually trivial, collectively often the largest single loss on a fast line, and almost never recorded by hand.
Blocking and starving – a station stopped because of its neighbour, not itself. Without line-level context this gets attributed to the wrong machine and the wrong fix gets funded.
Breakdowns – the visible failures. Already tracked in most plants, and usually a smaller share of lost time than the team expects.
Speed and changeover
Reduced speed – the line running below rated rate for reasons nobody logged, showing up only as a shortfall at the end of the shift.
SKU changeover – format parts, settings, line clearance and first-off approval. Measured per product pair, changeover becomes a scheduling input rather than a guess.
Start-up losses – the scrap and slow running in the first minutes of a run, which settings sent automatically to machines largely remove.
Quality and rejects
Rejects and rework – underweight fills, misapplied labels, failed seals and vision rejects, categorised at the station where they occur.
Labelling faults – labeller stops and speed loss correlated with the SKU and material lot running at the time.
Line clearance – verified and recorded electronically before the next SKU starts, which matters most in pharmaceutical packaging.
Shift reports vs a measured packaging line
The standard packaging report is written after the fact by someone who was busy running the line. Short stops are missing entirely, causes are guessed, and the number that reaches the morning meeting cannot be compared to yesterday because the definitions moved.
Once the line is connected, the same meeting starts from data nobody disputes: every stop timestamped and attributed, every changeover measured, OEE calculated the same way on every line in every plant.
Running on shift reports:
- Microstops invisible - the line "just runs slow" and nobody can say why
- Stop reasons written from memory hours later, if they are written at all
- OEE defined differently on each line, so cross-line comparison is meaningless
- Changeover duration estimated, so the schedule is optimistic by design
Running on measured production:
- Every stop captured from the PLC, including microstops of a few seconds
- Structured stop reasons, with the pattern behind repeat stops surfaced automatically
- One OEE definition across lines, plants and SKUs - genuinely comparable reporting
- Real changeover times per product pair feeding planning and sequencing
+5-10%
OEE gain on connected packaging lines
5 s
shortest microstop detected automatically
-20%
shorter SKU changeover after standardisation
24/7
live line status for every shift and site

“在该地区为该地区生产,贴近客户”是我们运营战略的支柱之一。近年来,我们对工厂进行了大规模投资,以扩大产能。.
借助所有制造系统中最佳的数字化解决方案来落实这些投资,是我们提升效率和敏捷性计划的关键组成部分。在与Accevo的紧密合作下,我们正在推进相关计划。.
维罗妮卡·奥托内洛
博米奥利制药公司 工业工艺工程师
What Accevo runs on a packaging line
One platform, connected once to each machine, feeding every module that needs the signal. Start with performance monitoring on the bottleneck line and add capability as the case is proven – up to a full 制造执行系统 if that is where you end up.
OEE & line performance monitoring
Availability, Performance and Quality calculated live from machine signals, per line, station, shift, SKU and order – with one definition that holds across every site.
微停机监测
Automatic detection of short, repeated interruptions, grouped and correlated so the bottleneck station and the pattern behind it become obvious.
Changeover management
Standardised changeover sequences with measured durations per product pair, plus automatic transmission of settings and formats to the machines.
Andon & maintenance calls
The line calls for technical, material or quality support directly from the station, with escalation and response time measured rather than assumed.
Shop-floor visualisation
Large-screen dashboards showing output against target, current status and OEE, so the whole crew sees the same number at the same time.
Dashboards & reporting
Ready-made reports for stops, output, rejects and efficiency, exportable to Excel, with aggregated and detailed views available in seconds.
Find out where your current packaging process fails
Request a compliance gap assessment and get a clear action plan to address the risks.
OEE for packaging lines, done properly
OEE tracks Availability, Performance and Quality. In packaging it is used above all to reduce stop-related losses and stabilise throughput by making the losses measurable and comparable. The value is not the percentage – it is that a falling percentage always decomposes into a specific, costed cause.
Line-level, not just machine-level
A packaging line is a chain. Measuring each machine in isolation attributes stops to whichever station happened to halt, not to the one that caused it. Accevo models the line, so blocking and starving are separated from genuine faults and the real constraint is identified.
Context that makes comparison fair
Performance is tracked by line, station, shift, SKU and order. That is what lets you ask whether this SKU is genuinely harder to run or whether one crew has found a better method worth standardising.
From measurement to action
Losses are ranked by minutes and cost on a Pareto and loss tree, converted into owned actions with deadlines, and re-measured afterwards – closing the loop that most monitoring projects leave open. See our continuous improvement tools.

Labelling, coding and serialisation on the line
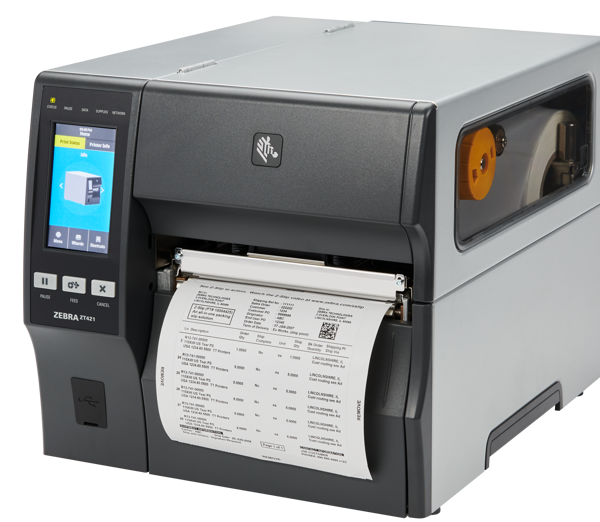
Labelling is where packaging lines quietly lose both output and compliance. A labeller that stops six times an hour barely registers on a shift report, but it caps the whole line – and in regulated packaging a mislabelled unit is a far more expensive event than a stop.
Accevo Pharma MES 正是为应对这一现实而打造的——批量处理、LIMS 集成以及跨药品、疫苗、膳食补充剂和化妆品的实时质量检查。您可以基于真实的生产数据做出决策,并将其与公用设施的使用情况进行关联分析。.
Labeller stops and speed loss
Labelling-related performance is tracked in its own right, with labeller stops correlated against SKU, material lot and line speed so the cause is identifiable rather than merely visible.
Structured stop reasons
Operators pick from a defined reason set rather than free text, which is what makes the data aggregable across shifts, lines and sites instead of being a pile of comments.
Coding, serialisation and track & trace
Serial number flow between packaging lines and enterprise level for anti-counterfeiting and regulatory compliance, with aggregation handled in the same system.
Integration with the systems you already run
Packaging monitoring is only useful if it carries production context, and that context lives in your WMS and ERP. Accevo delivers the integration as part of the project rather than leaving it as your problem.
WMS integration
ERP整合
Automation and control systems
Line states, counts and alarms read directly from the controllers: OPC UA, Siemens S7, Allen-Bradley, Modbus TCP, EtherNet/IP and others.
End-to-end delivery
Our own automation engineers do the connection work, including gateways, sensors and edge devices where a machine exposes nothing useful. No separate integrator to coordinate.
Built for the way packaging plants actually work
The system has to be useful during the shift, not only in the monthly review. That means clear line status, honest stop analysis and a small number of KPIs people trust – and it means starting on one line and standardising outward rather than launching a plant-wide programme and hoping.
快速消费品包装
Stable throughput at speed, with stop patterns detected fast enough to act on within the run.
Pharmaceutical packaging
Disciplined monitoring, electronic line clearance and structured evidence for investigations.
化妆品包装
High SKU counts and sensitive stations, where disturbance detection matters more than raw speed.
Built for every role on a packaging line

Production Line Manager
Know which station is constraining the line right now, not at the end of the shift – and have the stop data to argue for the fix with numbers rather than impressions.

持续改进领导
Every interruption captured and categorised automatically, ranked on a Pareto, so a Kaizen event starts with the top three losses instead of a fortnight of manual data collection.

Operations Director
One OEE definition across every line and plant, making cross-site benchmarking honest and turning the best-performing line into the standard the others are held to.
Start with one line, standardise, then scale

常见问题解答
Packaging industry software, explained
OEE tracks Availability, Performance and Quality. In packaging it is used mainly to reduce stop-related losses and stabilise throughput by making losses measurable and comparable across lines, shifts and SKUs. The value is in the decomposition: a falling OEE always resolves to a specific, costed cause.
By tracking stop frequency and duration per station, structuring stop reasons so they can be aggregated, detecting microstops automatically from PLC signals, and showing trends over time so the improvement team can prioritise by measurable impact rather than by impression.
A microstop is a brief interruption - often only a few seconds - caused by a jam, misfeed or momentary starvation. They are too short to log by hand, so they rarely appear in downtime reports, yet on fast packaging lines they are frequently the largest single loss in the plant.
The focus of this page is OEE and packaging line performance monitoring rather than full MES execution. That said, the modules run on the same platform, so plants that later need order execution, traceability or electronic records can add them without changing system.
Yes. Accevo exchanges production information - order IDs, quantities, statuses and timestamps - with WMS for warehouse processes and reporting, and integrates bidirectionally with ERP including SAP. Integration is delivered as part of the project.
Yes, per product pair. Changeover sequences are standardised and their real durations measured, which turns changeover from an assumption in the schedule into a number - and identifies which transitions are worth attacking first.
Yes. Most machines with an existing PLC or SCADA need no new hardware. Where a machine exposes nothing useful, our automation engineers add counters, sensors or I/O modules and wire them themselves.
FMCG and food, pharmaceutical, cosmetics, beverages and tobacco packaging, plus converters and co-packers. The line behaviour is similar across all of them; what differs is the compliance layer on top.
相关文章
利用数字化解决方案优化制造业包装
In the manufacturing industry, packaging is crucial for ensuring product integrity, enhancing brand image, and improving customer satisfaction. However, traditional packaging processes can be inefficient and prone to errors. Digital solutions are transforming how packaging lines operate, boosting efficiency, and reducing downtime. Digital Solutions in Packaging Digital solutions like Manufacturing

如何在 3 个月内实施无需验证的 OEE 监测系统?- 案例研究。
The pharmaceutical industry is one of the most demanding manufacturing industries. The combination of high process efficiency associated with the high volume of medicines produced, while maintaining the highest quality standards in compliance with strict regulatory standards, plays an important role here. An effective way to maintain high production efficiency
通用主批次记录 (GMBR) 如何提高包装效率
In the pharmaceutical and manufacturing industries, Generic Master Batch Records (GMBRs) are increasingly being used to improve packaging efficiency. GMBRs are a type of master batch record that groups together similar workflows, reducing the number of individual MBRs required. This can lead to significant savings in time and resources, as